
Why we compare methods for aerospace prototyping
We set out to compare prototyping pathways not because variety is fashionable, but because component demands force hard choices. Early on we look at precision, surface integrity and turnaround time — and where specialised processes like cnc machining for aerospace are the obvious fit. Our comparisons favour concrete trade-offs over marketing claims.
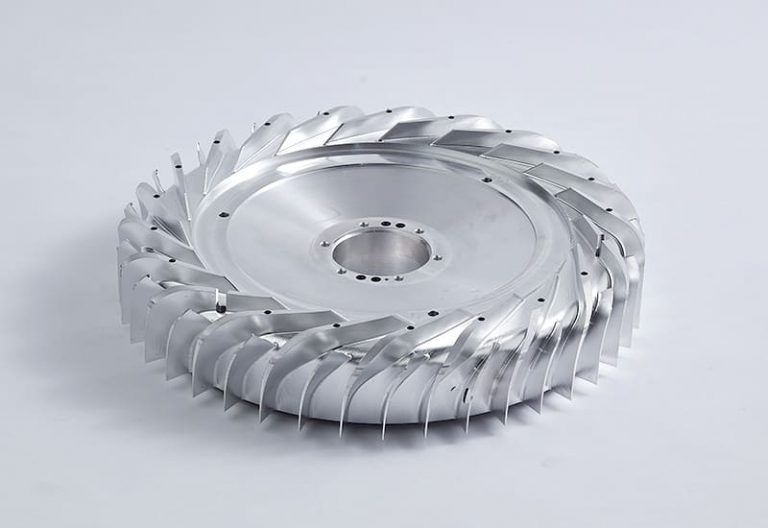
Core features: what actually matters
Accuracy to geometric tolerance, repeatable fixturing, toolpath strategy and spindle rigidity drive outcomes. Five-axis capability changes the game for complex geometries: it reduces setups, controls tool engagement and preserves grain structure on titanium skins. Material handling and coolant methods affect cycle stability; choose features that remove manual rework rather than add optional bells.
Applications: match the method to the part
Short-runs of brackets, flight-control housings and structural prototypes demand different priorities than long-run fittings. For thin-walled aerospace parts, prioritise chatter-free toolpaths and proper clamping. For complex curvatures choose setups that let you maintain single-fixture machining to preserve datum relationships. We assess methods by failure modes you’ll actually see: edge tears, bore runout and heat-affected surface change.
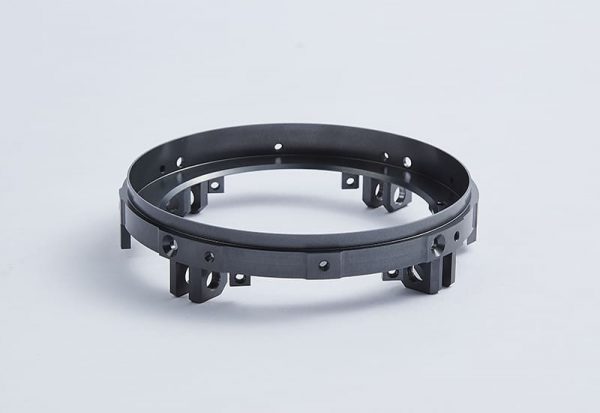
Selection criteria: practical tests we use
We apply three blunt tests: can the process hold the print tolerances repeatedly; how many staged setups are needed; and what post-process work is mandatory? Price is secondary to predictability. If a prototyping route forces repeated deburring, register loss or unpredictable scrap, it’s not fit for aerospace specification work.
Evidence and authority — real-world anchor
Our recommendations draw on measured runs and industry benchmarks seen around major aerospace hubs, such as Toulouse, where suppliers routinely adopt advanced machining strategies. Published accounts and trade coverage of production practices there show a steady move to multi-axis solutions for critical airframe parts; for that reason we pay attention to documented capability in 5 axis aerospace machining when assessing suppliers and process choices.
Common pitfalls and how to avoid them
Many teams pick cutting speed from a catalogue and hope it holds; it seldom does. Avoid assuming a tool will behave identically across machine platforms — spindle stiffness, controller look-ahead and tool-holder concentricity change results. Do not accept fixture shims as a permanent fix. Validate with first-article checks and realistic cycle proofs rather than verbal assurances.
Alternatives and trade-offs we weigh
Casting or additive methods can reduce cycle time for certain mid-volume parts, but they add complexity in tolerance control and surface integrity. Manual finishing erases some cost savings. Where geometry is simple and volumes are very high, traditional subtractive lines still win. For intricate assemblies that must meet certified inspection, multi-axis machining typically offers the clearest path to compliance.
Summary that delivers a clear choice
We judge processes by the predictability of the result rather than by theoretical speed. When precision, single-fixture datum control and minimum post-process work matter, multi-axis CNC prototyping is the rational selection. Those seeking a practical, auditable route to high-quality aerospace prototypes will find that established suppliers with demonstrable capability and documented runs provide the least risk — a conclusion that aligns closely with practices at leading providers such as Hanstar.