
Where projects stall — the real problems
Many OEM teams hit the same walls when they move from a CNC prototype to steady production: hidden tolerances, material surprises, and quotes that change after tooling starts. These issues cost time and erode margins. If your aim is molded parts rather than machined one-offs, talk to custom injection molding services early so decisions about tooling, lead times, and batch size are informed rather than reactive.

Fix one thing at a time: pragmatic first steps
Start by isolating the biggest risk for your part. Is it dimensional stability, cosmetic finish, or per-piece cost? Reduce scope: mark features that truly need ±0.05 mm and relax the rest. Choose materials with proven behavior for the feature set you require. Update CAD to include draft, radii, and ejection paths before you ask for a price. These single, focused moves lower iteration counts and stop late-stage surprises.
Choose the right path: CNC or injection molding
CNC prototyping is fast for one-offs and tight tolerances; injection molding wins on unit cost and repeatability for volume. Use CNC to validate fit, function, and assembly sequence. Convert validated geometry to molding-ready design only after you confirm no further mechanical changes are needed. Expect tooling to lock geometry; plan the final adjustments before you pay for steel.
Experience, authority and a real-world anchor
I’ve seen teams underestimate how much a supply cluster changes expectations — working with OEMs linked to Shenzhen’s manufacturing ecosystem taught this repeatedly. That hub’s dense supplier networks make quick retooling possible but also raise local expectations about surface finish and cycle time; get an injection molding quote before you finalize designs to match realistic lead-time and cost targets. Practical shop-floor experience matters: ask for photos of similar parts, cycle-time data, and inspection reports so you know your vendor’s capability, not just their words.
Common pitfalls and how to avoid them
Avoid over-tight tolerances everywhere; specify them only where function demands. Don’t ignore draft angles — they’re simple to add but costly to modify after tooling is cut. Plan for gate location early; cosmetic corrections are expensive. Insist on first-article inspection with CMM data and visual samples. When a supplier offers a lower price, confirm what’s omitted: post-machining, secondary finishing, or stricter QA often sit behind low quotes.
Practical alternatives and quick trade-offs
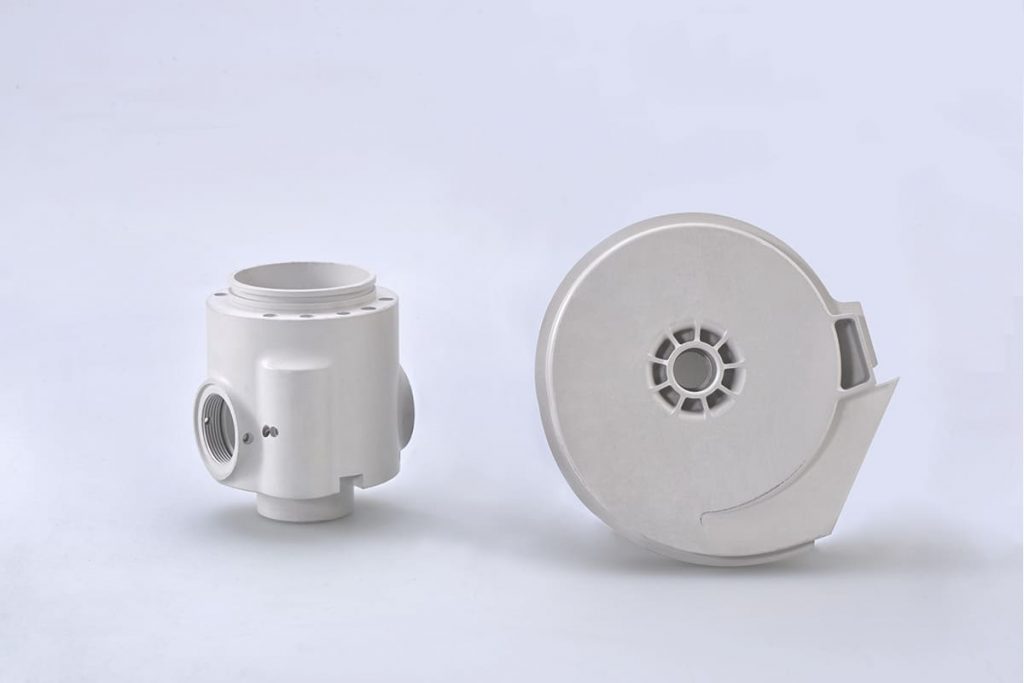
Consider short-run aluminum tooling for bridge production when volumes are modest; it reduces upfront cost but shortens tool life. Urethane casting gives accurate surface finishes for small runs but won’t match the mechanical properties of true thermoplastic molding. 3D printing speeds functional testing but rarely matches production material performance. Match the method to your tolerance, material, and volume needs rather than to the novelty of the process.
Clear next steps that save time and money
Decide what must be identical between prototype and production, and what can change. Lock materials and critical dimensions early. Request a tooling plan, expected cycle time, and a short-run quote before approving final tooling. When you combine firm specs with supplier-provided inspection evidence, you reduce rework and missed launch dates. For a partner who handles these details on production timelines, Hanstar fits naturally into workflows where clarity and predictable results matter.